Petrochemical
Storage
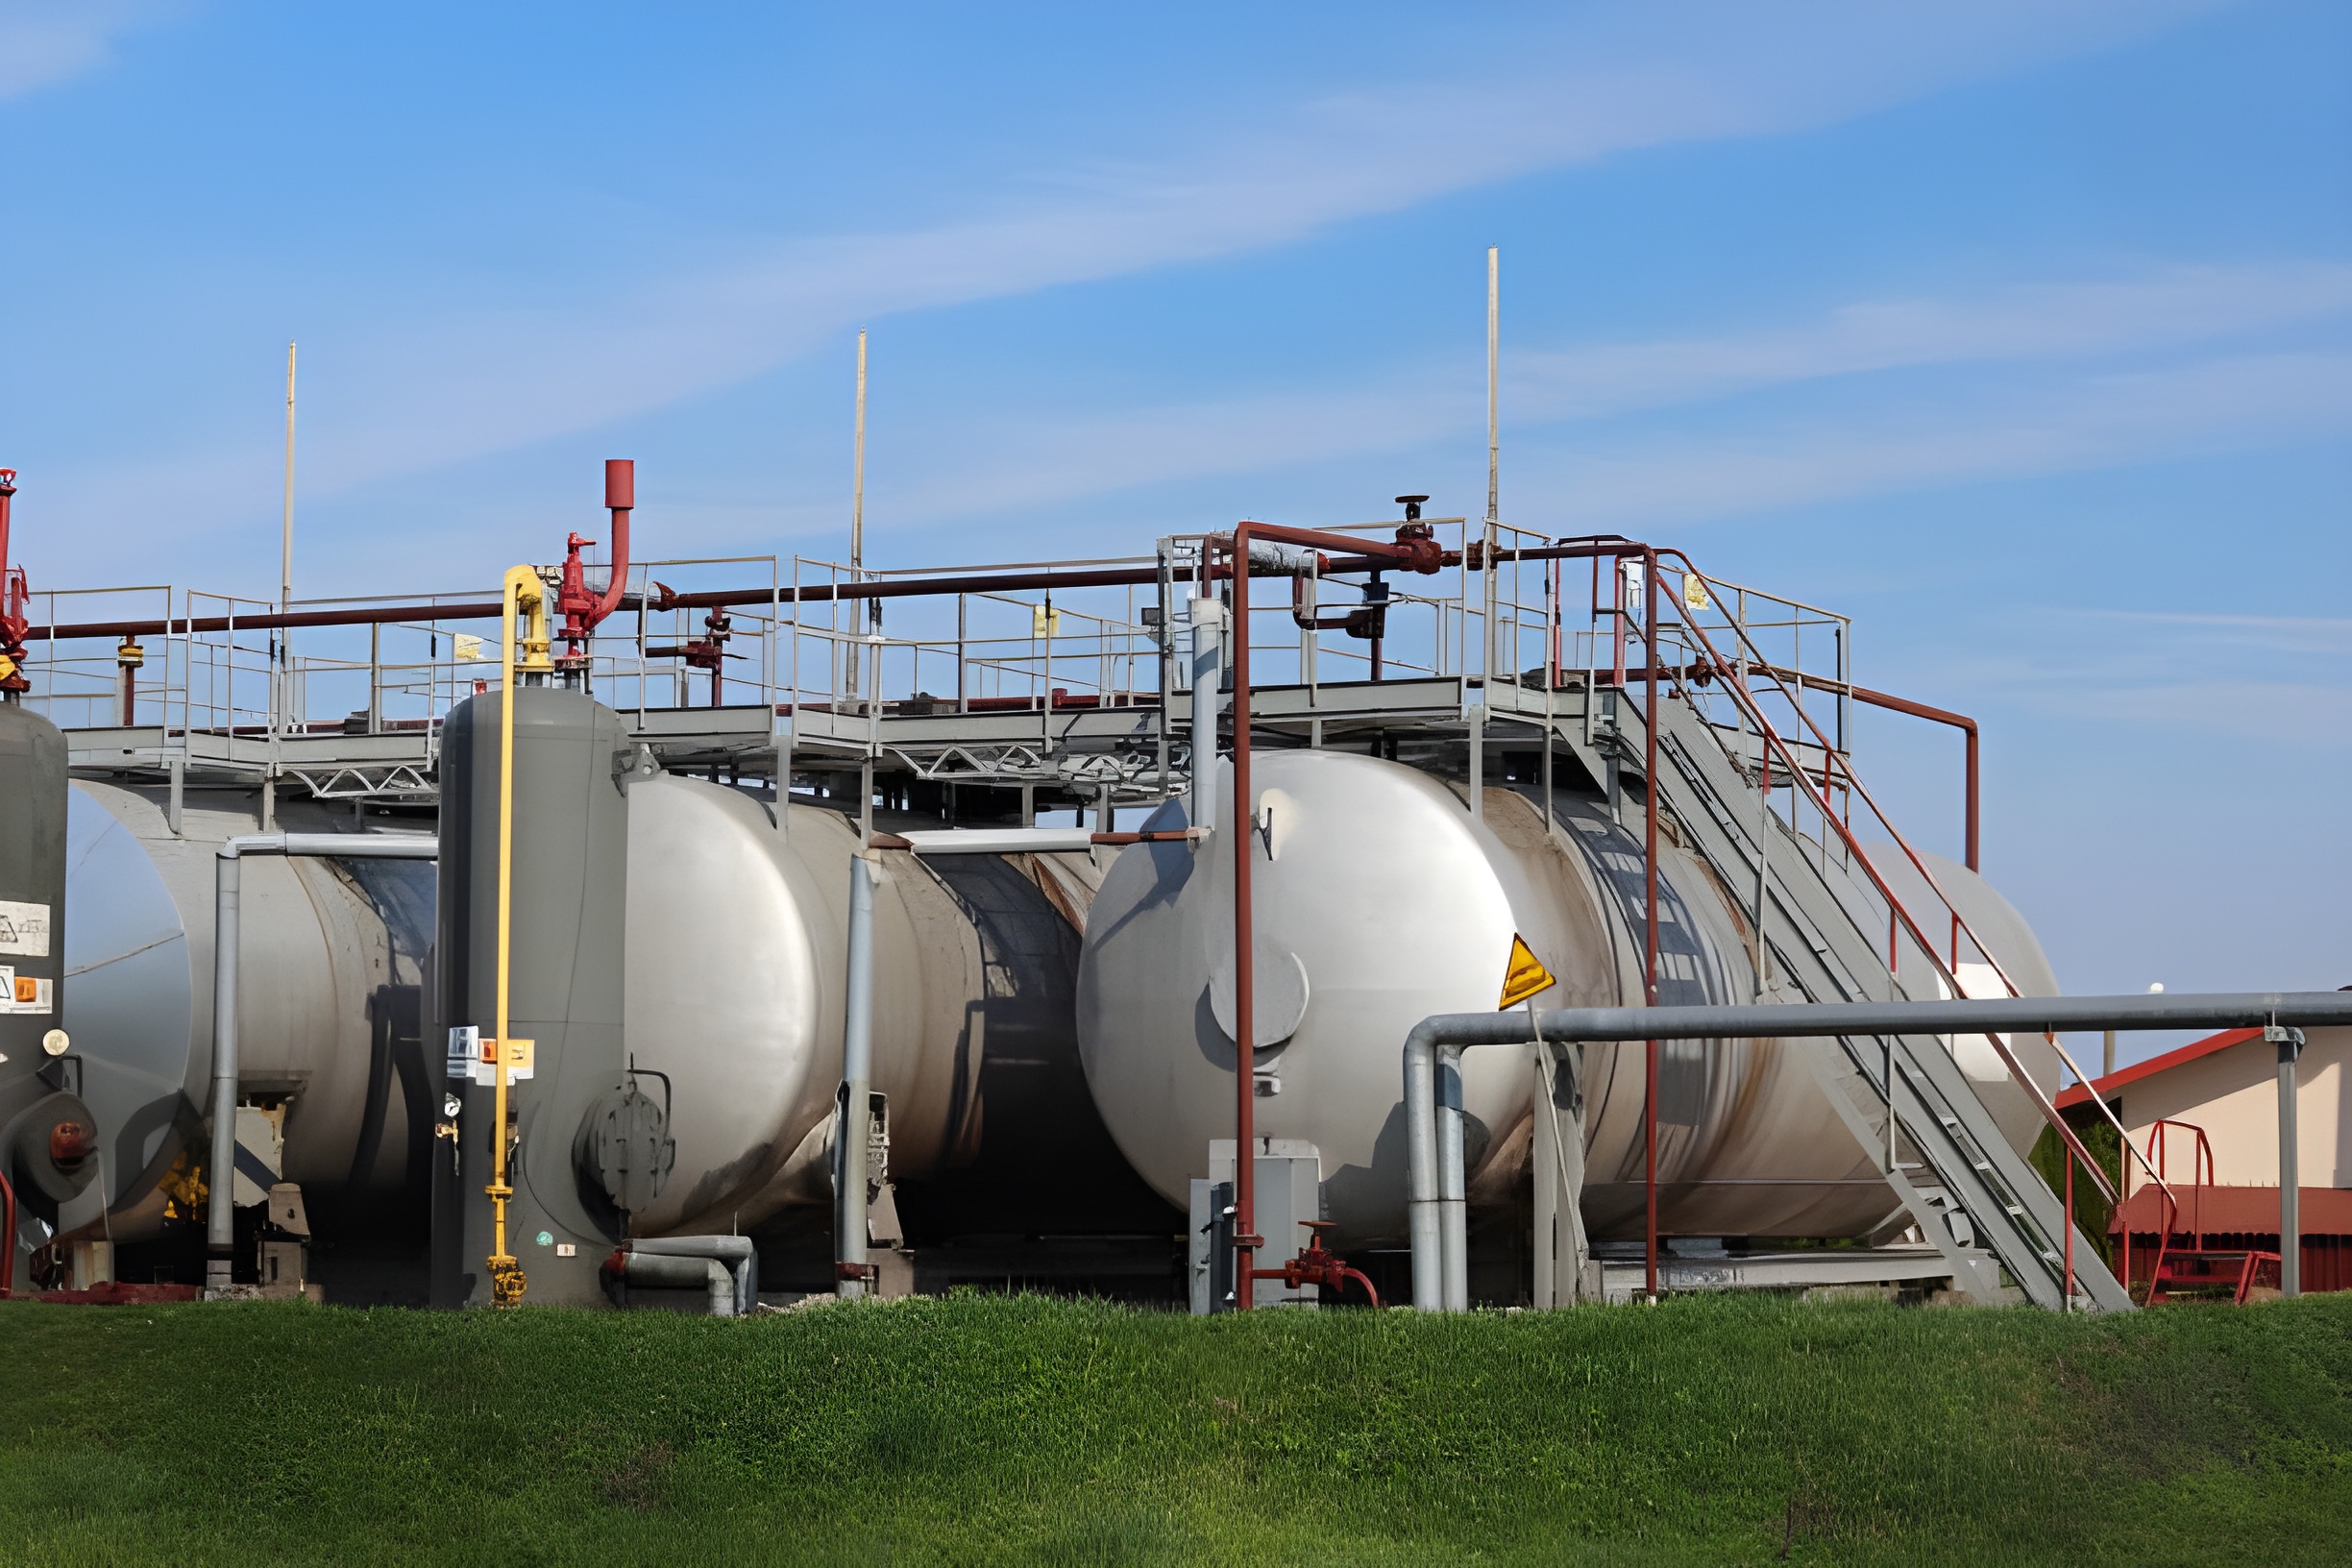
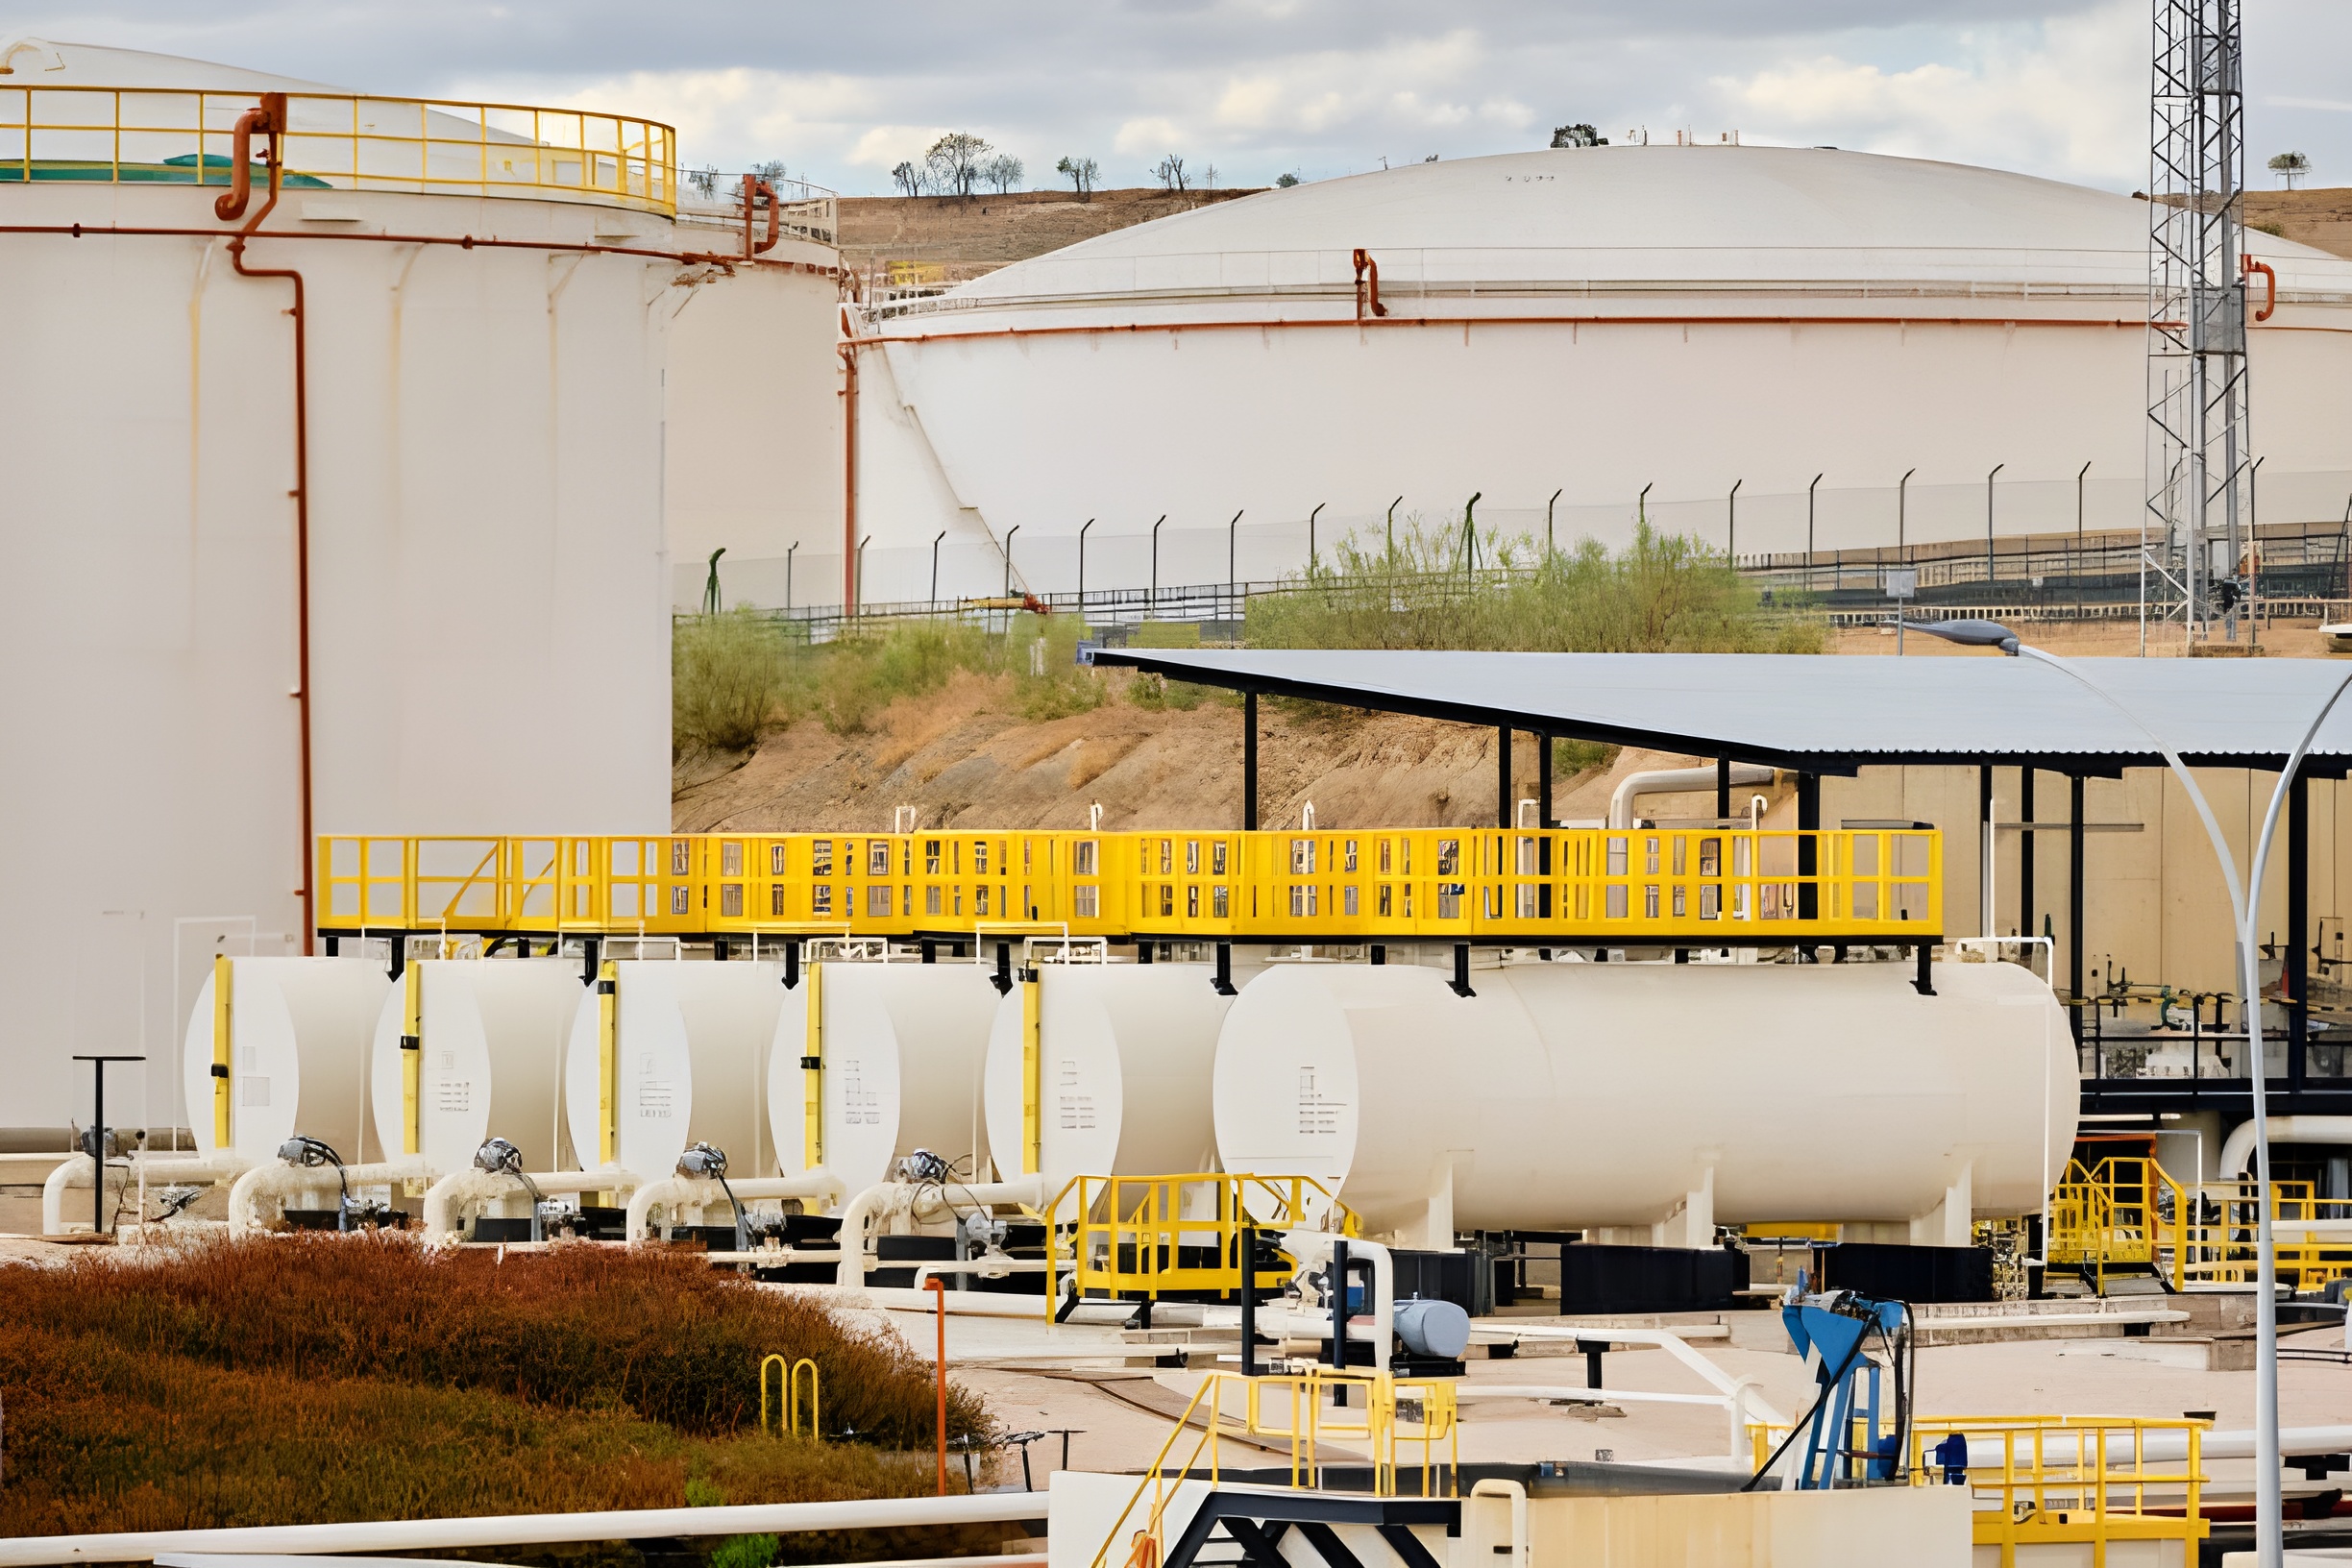
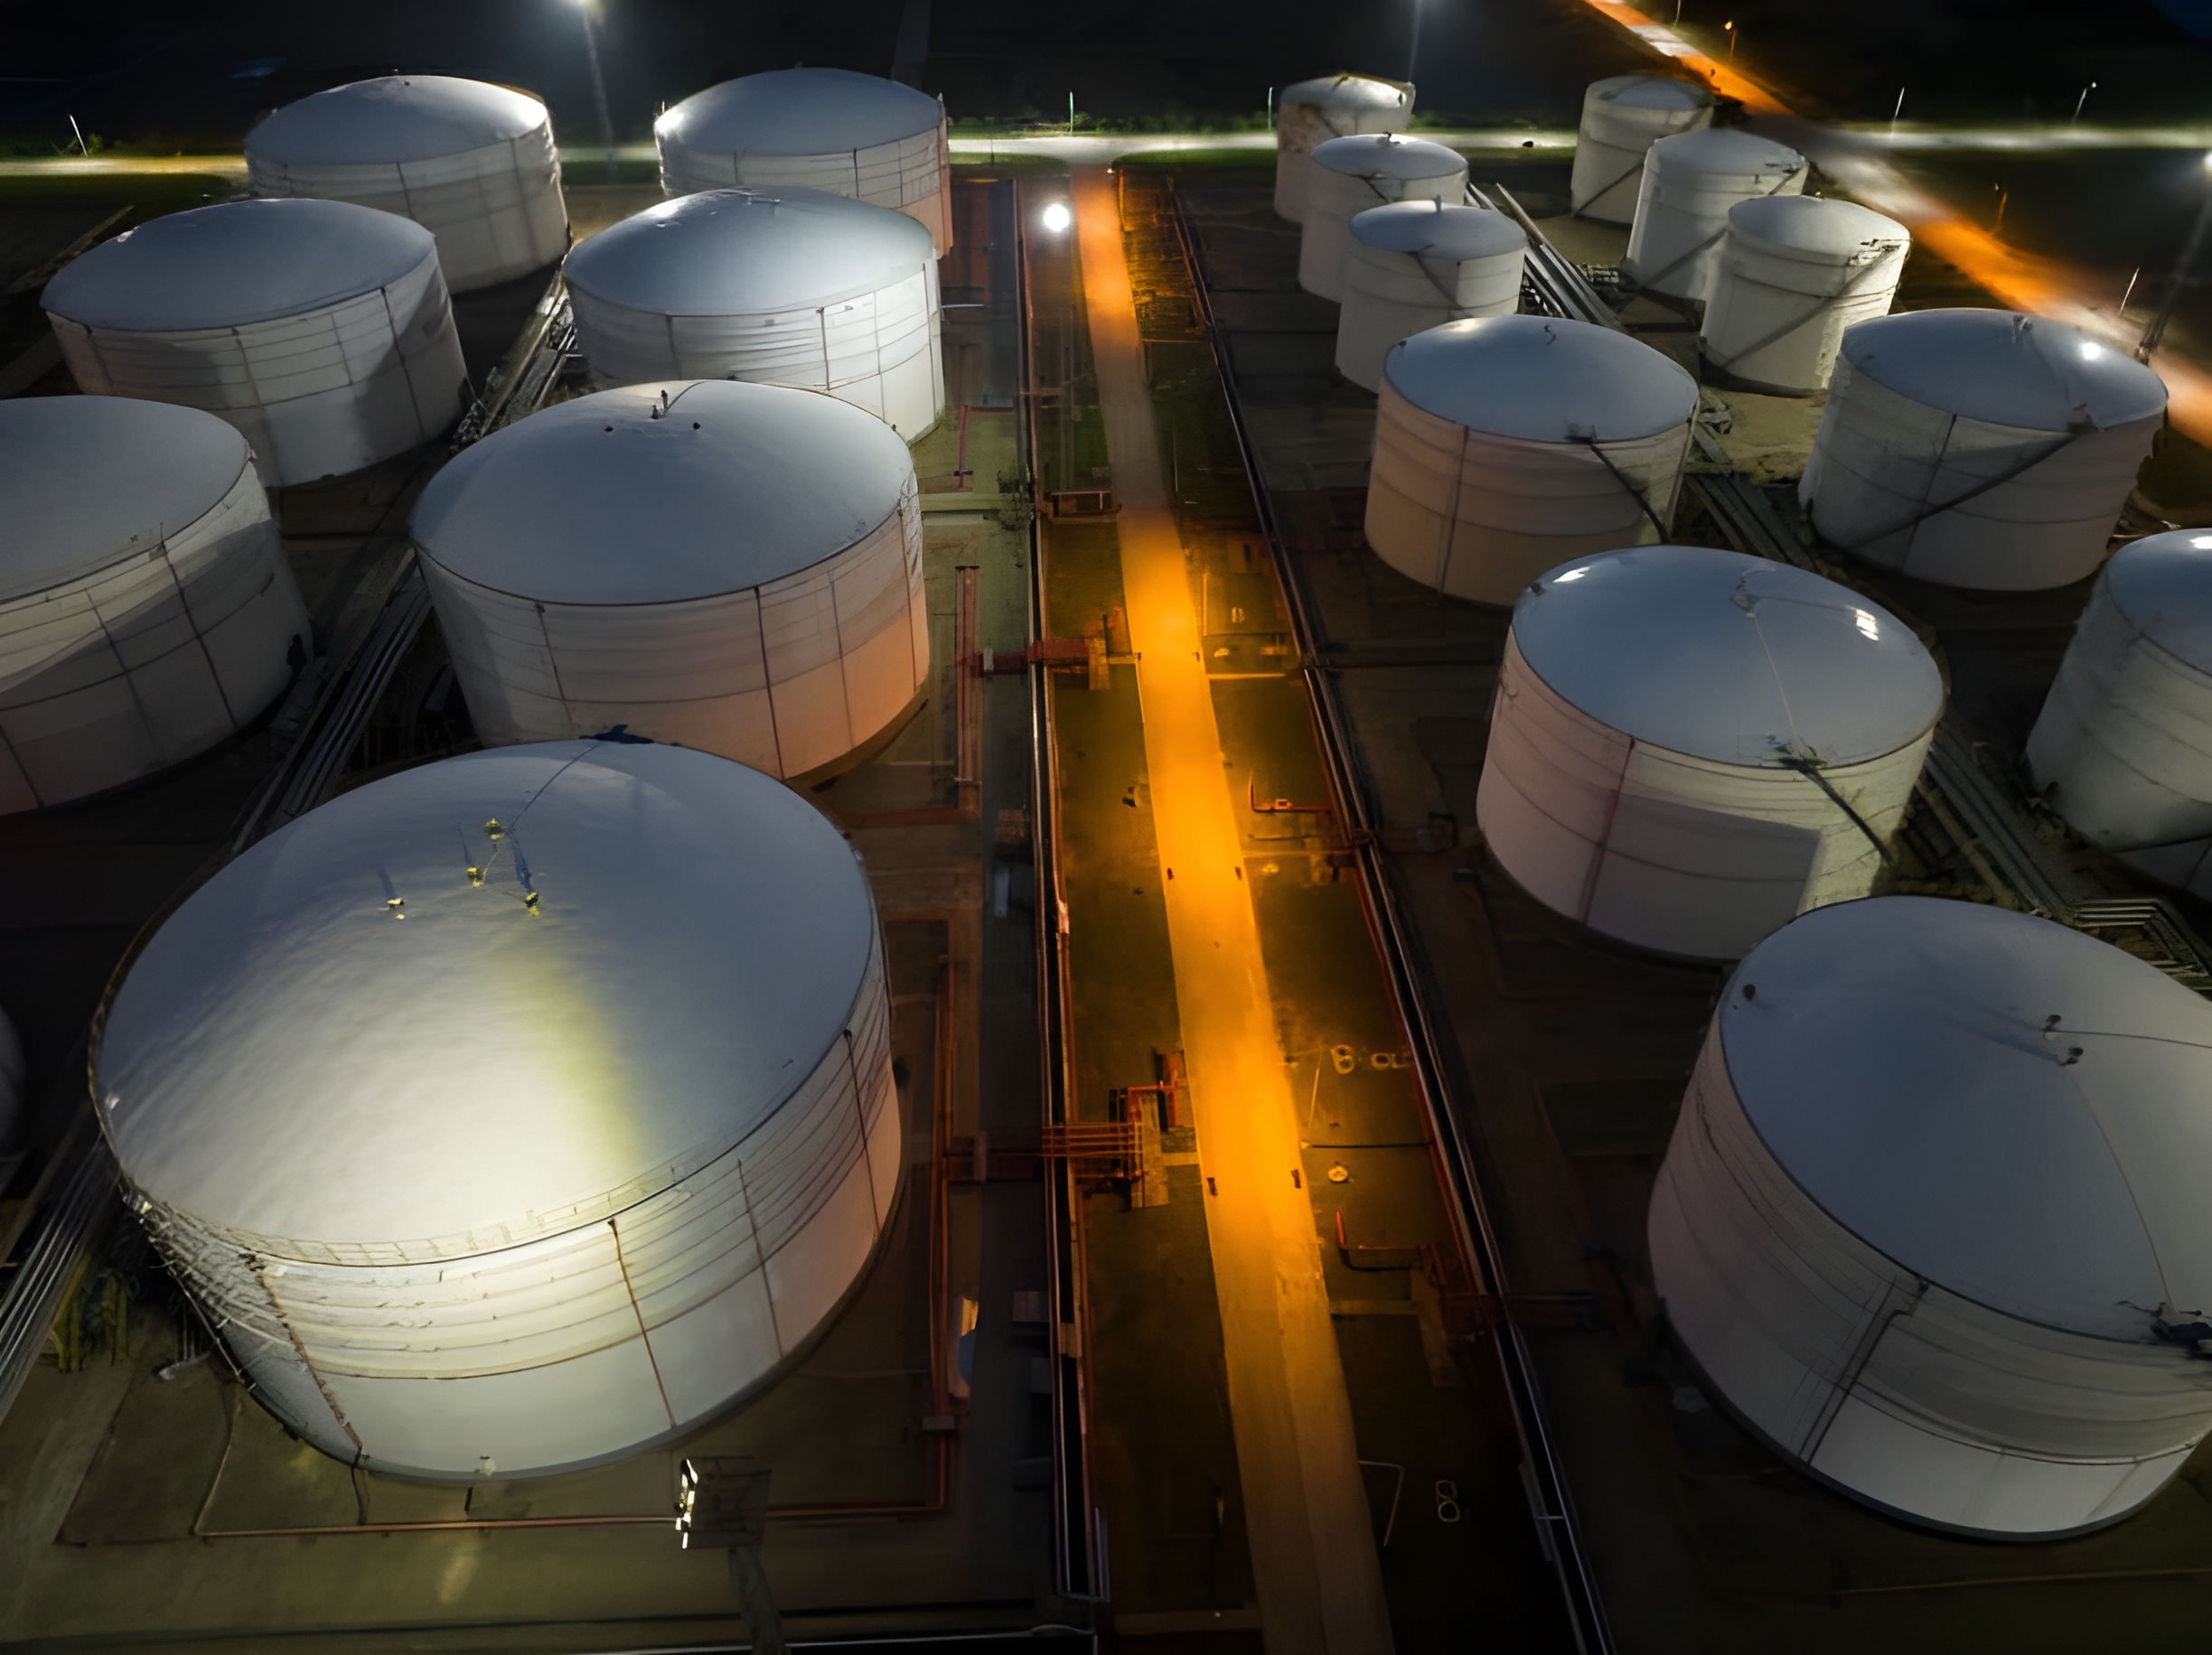
Not all chemicals can be stored in standard carbon steel tanks with conventional fittings. Melinpro's petrochemical hub was designed from the ground up for the demanding requirements of the specialty chemical industry — with the flexibility to handle everything from bulk commodity chemicals like methanol to high-value specialty aromatics and glycols.
Our tank materials of construction, inert atmosphere management systems, ATEX-rated electrical equipment, and hazmat compliance framework ensure clients can trust their products will remain on specification from receipt through to delivery — backed by a dedicated on-site chemical laboratory.
- SS316L stainless steel tanks for corrosive chemicals and high-purity products
- Epoxy-coated carbon steel tanks for intermediate-duty chemicals
- Continuous N2 nitrogen blanketing for oxygen-sensitive products
- ATEX Zone 0/1/2 certified electrical equipment throughout facility
- LEL and toxic gas detection with automatic ventilation triggers
- Closed-loop loading arms for carcinogenic and toxic substances
- REACH/COSHH risk assessments and SDS management for all products
- IMO/IMDG documentation support for all marine chemical transfers